
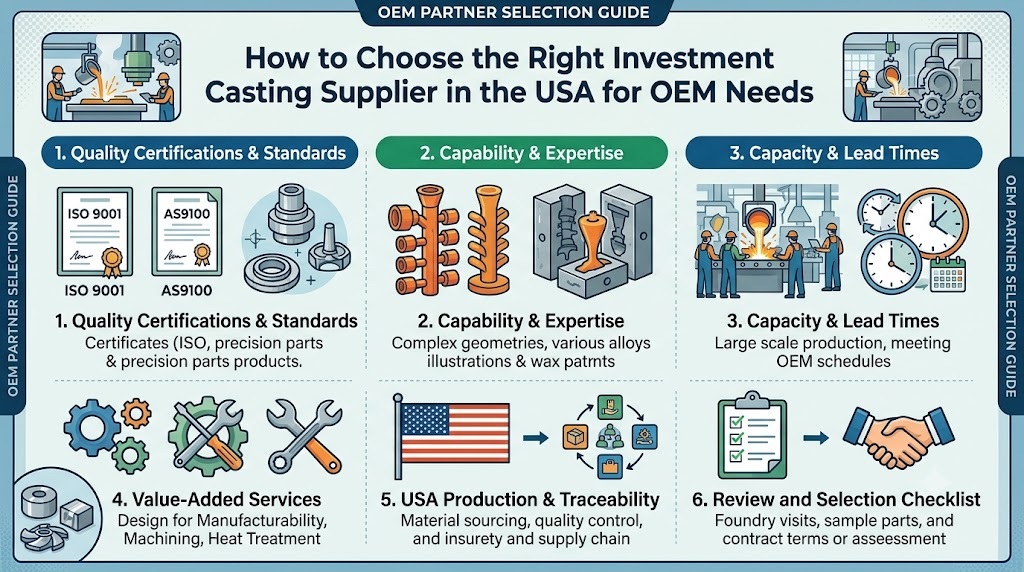
Finding a manufacturing partner is not about ticking a box in the procurement process; it signifies whether you will have a smooth-running production line or a series of costly, last-minute “emergency” meetings. In the niche world of Original Equipment Manufacturers (OEMs), the decision of locating the reliable investment casting suppliers USA comes hand in hand with your organization’s growth potential.
The “Aha” Moment: When Certifications Aren’t Enough
I hold a memory of a massive industrial pump housing project geared for a leading energy client a few years ago. Our “due diligence” was impeccable or at least we thought so. We selected a supplier from the US market who had all the proper ISO certifications. Their price was reasonable, not suspiciously low, just… comfortable.
The first batch of 50 units reaching us was a blast from the future in a way. They appeared flawless at the first glance. However, the moment we subjected them to a CNC for final boring, the issue was obvious. Porosity. It was not just in one or two pieces, but the entire batch. The supplier’s “quality control” had only measured the dimensions and unfortunately skipped the NDT non-destructive testing because “it was not specifically indicated in the RFQ.”
The hard truth I took away that day was that a supplier is only as good as the questions antecedent to the contract signing. The USA market is a very sophisticated one, but it is also highly niche. A foundry is not what you need; you need a partner who knows your specific metallurgical requirements and tolerances very well.
Why Investment Casting for OEMs?
Investment casting (also called the “lost wax” process) is the most accurate methodology for the production of complex, near-net-shape components. For OEMs, it is an invaluable way to minimize secondary machining and material waste.
- Cool shapes? Yep – mold tricky insides and slim walls no sand method can handle, ’cause it’s just stuck on simpler forms.
- Surface Finish: We’re talking about as-cast finishes of 32–63 µin Ra – smooth enough that many parts are “ready to use” out of the box.
- From common 316L steel to high-performance cobalt alloys, options stretch far – thanks to wide adaptability.
1. Audit the “Invisible” Capabilities: Beyond the Pour
When one is on the hunt for investment casting suppliers in the USA, most buyers tend to zero in on the melt capacity. To be honest? That is the simple part. Real differentiators lie in engineering and post-cast services.
In-House Engineering and DFM
Is the supplier harboring a design team internally? You expect individuals who will analyze your CAD file and propose, “If the fillet is moved 2mm, scrap rate will be cut by 15%” called Design for Manufacturability (DFM).
- Try asking whether they run solidification simulations. That kind of tool helps spot weak zones and shrinking risks way before any wax gets poured – so you’re ahead from the start.
Secondary Operations: The “One-Stop-Shop” Advantage
Just imagine, it’s a nightmare in logistics to send a bare casting from the foundry to a heat treater, then to a machine shop, and eventually to the player. Each “hand-off” is a chance for a delay or a quality dispute.
- The aim? Track down a vendor that handles everything – heat treating, precise CNC work, or surface finishes. This way, your supply chain gets easier while responsibility stays clear. When something breaks, you’ve got just one contact to ring up.
2. Navigating the “Alphabet Soup” of US Quality Standards
The US market is under the watch of heavy regulations, especially if one is operating in Aerospace, Medical, or Defense. You should confirm that your investment casting suppliers USA are not only “complying” with the standards but also being certified by independent third parties.
- ISO 9001:2015 – start here. Without it? Just leave. But if they’ve got it, maybe listen. Still, check everything else first. Because one certificate doesn’t fix flaws. So stay sharp.
- AS9100 matters a lot in aviation and military work – it pushes further than ISO standards by demanding tighter controls while focusing on risk oversight instead of just basic compliance.
- Nadcap Approval – this matters most when it comes to niche manufacturing steps. Parts needing certain inspections like X-ray or magnetic testing? Check for that Nadcap mark. Same goes if heat treatment’s involved – look for their stamp.
- Dealing with military parts? Then ITAR registration isn’t up for debate – it’s the law.
3. Speed and Quality, finding the right balance
Nowadays, speed is often the main factor distinguishing B2B brands from each other. However, in the field of investment casting, “rushing” almost invariably results in cracks or inclusions. It is a delicate balancing act.
Prototyping and 3D Printed Wax
Traditional production tools from scratch can take up to 6 to 12 weeks. What if you immediately want to have a functional prototype? Then, you should request 3D-printed wax models.
- You get parts fast – just days from CAD to finished metal piece – with no need to pay big money for a fixed mold up front. Great if you’re making small batches or testing how your design works before going all-in on mass production tools.
Automated Robotics
What sets apart the elite investment casting suppliers in the USA these days is their exponential pump of money in the automation efforts. The primary reason is that, unlike humans, robots never get tired and they are consistent with the time they spend dipping a part in the ceramic slurry.
- Every shell gets built the same way – robot arms spread material evenly, so walls stay steady when metal flows in.
4. Calculation of TCO (Total cost of ownership)
Let’s be honest about the pricing. The “per-piece” price on a quote is most of the time a lie – or at least just half of the truth.
Tooling: Expense vs. Investment
Different foundaries might have different charges and the real cause of this gap is mentioned below:
- One mold versus multiple molds: that 15k machine could make four pieces each time – so you save more cash over time while getting stuff done faster.
- Fine aluminum gear works well with auto injectors, so it keeps performing steadily through 10K rounds or more – thanks to solid build quality.
The Cost of a “Cheap” Part
| Factor | “Budget” Supplier | Tier-1 US Supplier |
| Initial Unit Price | Lower | Fair/Higher |
| Scrap Rate | 5% – 10% | <1% |
| Machining Prep | Heavy grinding required | Minimal/None |
| Lead Time Risk | High (Batching issues) | Low (Just-in-Time) |
Frankly, it appears to me that lots of OEMs are focusing on a $2.00 saving per part, only to be put in a situation later when they have to pay $20.00 for rework, late fees, and customer dissatisfaction.
5. Vetting Your Shortlist: Questions You Must Ask
Have a “candid” chat with the account manager before you sign the contract. And include the below mentioned details:
Asking questions about the product rolling timeline? And when someone says 8 weeks yet skips talking about how long tools need, that’s likely wishful thinking.
- Got your own NTD gear? When they ship x-rays offsite, tack on another ten to fourteen days per run.
- “What is your alloy purity verification process?” You want to hear “spectrographic analysis on every melt”.
- What’s your plan when orders suddenly jump? Check out JIT methods – they let production grow fast, no need to stockpile tons of goods.
Final Reflections: Choosing a Partner, Not a Vendor
Ultimately, picking an investment casting supplier USA from your list boils down to confidence. You are, in fact, entrusting them with your final product’s integrity.
I have witnessed many OEMs treat casting as a commodity. In fact, it is not. It is a highly technical craft being modernized with AI and robotics. A partner that would be as interested in the success of your pump, engine, or medical device as you are, is the one you should go for.
Summary of Actionable Advice:
- Check credentials upfront – skip shops that don’t clear your sector’s rules right away.
- Think about total costs – include waste plus extra shaping when deciding.
- Use tech that works – pick providers running sim tools or robots to keep results steady.
You are the only person who really knows your product. Don’t allow substandard casting to become your weak spot. Always go for quality, verify standards and have confidence in your project.